
 Personal Account


 Личный Кабинет

Plant for electric arc welding in an inert environment "USKS-27"

Plant for electric arc welding in an inert environment "USKS-27"
Description
Установка «УСКС-27» для автоматической и ручной дуговой сварки неплавящимся электродом в контролируемой среде
 Detailed information PDF
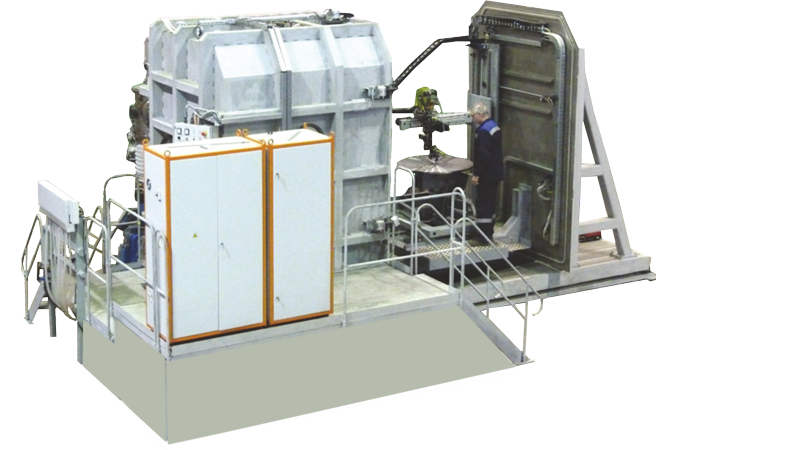
The "USKS-27" unit is designed for automatic and manual arc welding with a non-consumable electrode in a controlled environment of circumferential and longitudinal seams of products made of chemically active metals and alloys based on them, installed on the rotator faceplate, with or without filler wire.
The maximum diameter of welded products is 800 mm, the maximum height is 800 mm, the maximum weight of the welded product is 250 kg.
The unit allows welding in automatic mode with a welding head of butt, tee, overlap joints of bodies of revolution with a horizontal axis of rotation in various positions of the head - from vertical to turned at an angle of ±45 ° from the vertical. When the axis of rotation is set to a vertical position, it is possible to weld end joints of bodies of revolution with a vertical position of the head. The unit can be used to weld bends, fittings, plates, brackets, etc. to body parts using 150 A and 400 A manual welding torches. In automatic mode, welding of all joints can be performed with or without electrode oscillation. Butt joint welding can be performed with automatic maintenance of a given arc gap value.
The "USKS-27" unit is a chamber unit consisting of the following complexes: mechanical, vacuum, energy, automatic control system, air supply system, cooling system.
The working chamber contains: the welded product with equipment on the rotator faceplate and a mechanized welding head, two manual torches of 150 A and 400 A, installed on the sliding cover of the chamber.
Technical data
Overall dimensions of welded parts and assembly units (L*Ø*W), mm
800*800*800
Maximal weight of the welded product, kg
250
Inner dimensions of the vacuum chamber (L*W*H), mm
2000*2076*2984
Chamber volume, m3
12.4
Ultimate vacuum in the chamber, Pa (mm Hg)
6.6*10-3(5*10-5)
Vacuuming time, minutes
20-30
Time to fill the chamber with argon, minutes
1-3
Glove entries
4
Torches 150 A for manual welding, pcs
1
Torches 400 A for manual welding, pcs
1
Welding heads for automatic welding, pcs
1
Maximal welding current, A
400
Working coordinates of the manipulator
3
Angle of inclination of the axis of rotation of the rotator faceplate relative to the frame, °
0¸90
Maximal angle of rotation of the faceplate, °
±360
Faceplate rotation speed, rpm.
0.025-2.5
Longitudinal movement of the welding head console, mm
1110
Vertical movement of the welding head console, mm
545
Transverse movement of the welding head, mm
630
Vertical movement of the welding head, mm
230
Transverse movement of the rotator, mm
200
Automatic arc welding speed, m/s
0.0014 - 0.017
Filler wire feed speed, m/s
0.0028 - 0.028
Diameter of tungsten electrode, mm
16
Filler wire diameter, mm
1.2; 1.6; 2.0
Electrode oscillation amplitude, mm
±1¸ ±5
Electrode oscillation frequency, Hz
25
Controlling the movement of the rotator with the product and the tilt of the faceplate
from the welder's console
Turning on the power supply, adjusting the current
from the welder's console or foot pedal
Enabling longitudinal, transverse and vertical movements of the welding head
from the welder's console
Power consumption, kW
50
Overall dimensions of the plant (L*W*H), mm
7465*6160*3950
Detailed information PDF
Submit an inquiry
Прошлое
Настоящее
Будущее