
 Personal Account


 Личный Кабинет

Plant for welding longitudinal joints of sheets and shells "USPO-1.2"

Plant for welding longitudinal joints of sheets and shells "USPO-1.2"
Description
"USPO-1,2" plant for automatic non-consumable electrode welding of longitudinal joints of sheets and shells
 Detailed information PDF
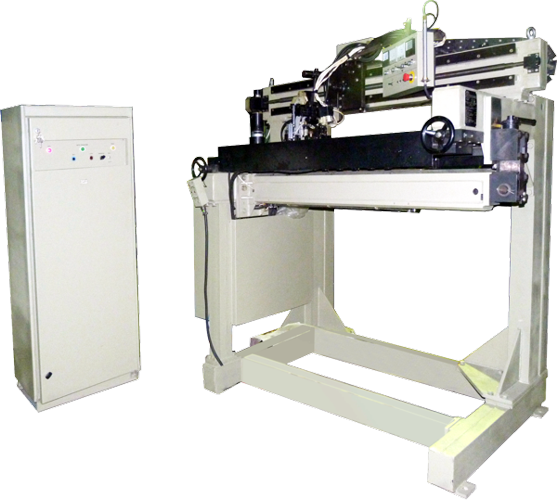
Welding on "USPO-1,2" is carried out with a continuously burning or pulsed arc of rectified direct current. Non-consumable electrode welding (also gas shielded non-consumable electrode welding) is a type of welding in which the heat source is an arc discharge that occurs between a tungsten electrode and the product. This type is a variation of fusion arc welding methods. This technology is mainly used for processing aluminum, magnesium and their alloys, as well as other non-ferromagnetic metals (for example, stainless steel, bronze, copper, zirconium, nickel).
With the automated version, both the movement of the welding torch and the supply of filler material (wire) are completely mechanized. The technological process is controlled by the operator.
When welding with a non-consumable electrode, direct current of direct polarity is used, since in this mode the maximum penetration of the metal of the parts that are to be joined occurs. This is achieved through efficient use of energy: up to 85% of thermal energy goes to melting parts, up to 7% to heating the electrode, the rest is radiation losses.
The main advantages of the "USPO-1,2" plant
1. Possibility of minimal deformation in the metals being welded due to the small heating zone;
2. High quality of connection due to the use of protective gases that displace oxygen;
3. Relatively high speed of work;
4. Minimum labor costs for subsequent processing of the seam;
5. Relatively wide range of weldable materials.
The "USPO-1,2" plant consists of the following assembly units, which are interconnected by mechanical and electrical connections:
- Supports left and right;
- Lodgment;
- Rear pressure beam;
- Front pressure beam;
- Guide beam;
- Lock;
- Pedal block;
- Welding head "ASGV-4ARK";
- Latch;
- Gas, water and electricity distribution;
- Gas control unit;
- Pneumatic system;
- Control system;
- Power supply “VSVU-400”.
Technical data
Rated supply voltage, V
400/230
Inner diameter of welded shells, mm
250 - 1200
Maximum length of welded sheet (shell), mm
1200
Thickness of welded material, mm
0.5 - 4.0
Welding speed control range, m/hour
5 - 40
Range of control of filler wire feed speed, m/hour
10 - 110
Filler wire diameter, mm
0.8 - 2
Diameter of tungsten electrode, mm
2 - 5
Burner installation movements, mm
100
Vertical speed of burner movement, m/s
0.005
Angle of inclination of the torch to the welding plane, °
±90
Rated welding current, A
350
Maximum power consumption, kW
28
Overall dimensions (L*W*H), mm
2350*1355*2274
Detailed information PDF
Submit an inquiry
Прошлое
Настоящее
Будущее