
 Personal Account


 Личный Кабинет

Vacuum induction melting furnace with a cold crucible "UPHT"

Vacuum induction melting furnace with a cold crucible "UPHT"
Description
Vacuum induction melting furnace with a cold crucible "UPHT" for producing of high-precision castings from polycrystalline materials and intermetallics
 Detailed information PDF
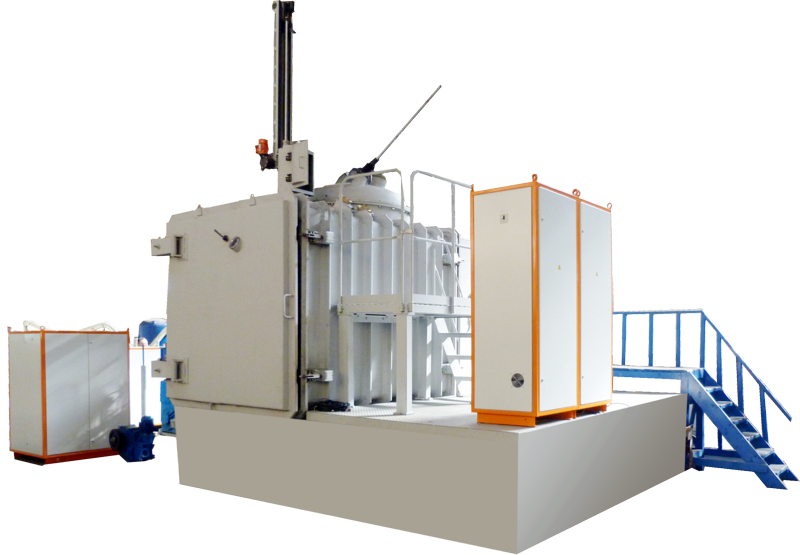
Vacuum Induction Melting Furnace with Cold Crucible "UPHT"
Purpose and Application
The vacuum induction melting furnace with cold crucible "UPHT" is designed for producing of high-precision castings from polycrystalline materials and intermetallic compounds.
UPHT Plant Components
- Melting Chamber
- 50 kg Melting Block
- Coaxial Power Supply
- Vacuum System
- Loading Device
- Centrifugal Device
- Mold Heating Furnace
- Pouring Device
- Water Cooling System
- Capacitor Bank
- Power Supply
- Rolling Block
- End Cover
- Top Cover
- Container
- Vacuum Control Cabinet
- Pneumatic System
- Rack
- Foundation
- Electrical Wiring
- Crucible Rotation Drive
- Gas System
- Loading Panel
- Mechanism Control Cabinet
- Operator Panel
- Power Cabinet
- Backup Emergency Water Cooling System
- Stand
Design and Operation of the Plant and Its Components
The plant produces high-precision castings from polycrystalline materials and intermetallic compounds. The system is designed as a vacuum chamber. One end of the chamber is closed by an end cap secured with pneumatic clamps, while the other end is closed by a sliding block on a trolley. A top cover, secured with bolts, is located on top of the chamber. A loading device and a vacuum port are also mounted on top of the chamber.
The chamber is equipped with four supports for mounting it on supports.
The chamber houses the melting unit and a coaxial power supply. Two viewing windows are located on top of the chamber: one for the operator to observe the melting process in the crucible, and the other for the operator to use when handling the crowbar.
The melting unit is suspended on two pivoting journals. The unit contains a sectional copper crucible, with magnetic field concentrators positioned around the inductor.
The melting unit is powered via a coaxial power supply. Cooling is provided via pressure and drain manifolds, shaped like a daisy.
The loading device loads the charge into the crucible and measures the temperature of the molten metal with an immersion thermocouple.
Pouring of the metal from the crucible into the ceramic mold is ensured by a crucible rotation drive.
A mold preheating furnace is located inside the chamber to maintain the mold temperature at 850°C.
The centrifugal unit consists of a table and a drive, mounted on independent foundations. The centrifugal drive consists of a frame, an electric motor, and a gearbox. The table is a disk on a vertical shaft. A container with a ceramic mold for pouring the metal is placed on the centrifugal unit table. Metal casting is carried out using one of three process methods:
- Pouring metal into a mold preheated in a preheating furnace;
- Pouring metal into a mold located on a centrifugal device;
- Pouring metal sequentially into several molds spaced at a specified pitch on a rotary table.
A rollback unit is used for servicing and operating the preheating furnace, centrifugal device, and mold container. The rollback unit is mounted on a trolley driven by a drive along a track. The unit houses the melting chamber cover and a lifting mechanism for lifting the preheating furnace and container. After lifting, the rollback unit, containing the filled molds and the preheating furnace, moves away from the chamber to unload the castings.
The vacuum system consists of two lines: a forevacuum line and a high-vacuum booster line.
The vacuum system includes a set of pipelines, oil vapor traps, valves, and measuring instruments. The pneumatic system operates the vacuum system's pneumatic valves, as well as the pneumatic clamps of the end door and sliding unit.
The water cooling system removes heat from all heat-loaded components and surfaces.
To ensure trouble-free operation of the complex, a backup emergency water cooling system is used.
The gas system supplies argon for process needs.
The unit uses a modern control system with functions for recording operating parameters and troubleshooting.
The unit is controlled using the following cabinets and control panels:
- Vacuum control cabinet;
- Mechanism control cabinet;
- Power cabinet;
- Loading control panel;
- Operator control panel.
The power supply and capacitor bank are located near the coaxial power supply.
A ramp and ladders are available for servicing the unit.
Technical data
Crucible capacity, kg
50
Inductor voltage, V
800
Inductor current, A
1000
Rated frequency, Hz
2400
Melt temperature, °C
1800
Working vacuum, Pa
1.33* 10⁻³
Melting time, h
3
Inert gas pressure, Pa (mmHg)
0,9*10⁵ (700)
Installed capacity, kW
1190
Power supply voltage, V
400
Rated frequency, Hz
50
Footage, m²
85
Weight, kg
49000
Detailed information PDF
Submit an inquiry
Прошлое
Настоящее
Будущее