
 Personal Account


 Личный Кабинет

Vacuum single-chamber melting and pouring plant with preliminary heating of molds "VIPE-3R"

Vacuum single-chamber melting and pouring plant with preliminary heating of molds "VIPE-3R"
Description
Vacuum single-chamber melting and pouring plant of the "VIPE-3R" type with preheating of molds for the manufacturing of castings from heat-resistant alloys and steels
 Detailed information PDF

1. Purpose. Technological processes used.
The "VIPE-3R" plant is intended for the manufacturing castings from heat-resistant alloys and steels in mass production conditions. Casting method - lost wax casting. The range of castings includes equiaxial, small-sized, shaped and body parts made of heat-resistant alloys and steels. Casting block dimensions are up to 370 mm.
2. Features of the physical processes used.
Features of the "VIPE-3R" plant - a single-chamber plant, the ability to fill up to four molds per hour. The temperature of the metal is controlled by pyrometer within the melting process. Data from photopyrometer and immersed thermocouple pass to the monitor. The physical process is a result of magnetic induction.
3. Technical description. Design features. Advantages.
The "VIPE-3R" plant includes the following main components:
- Melting chamber,
- Door,
- Induction oven,
- Mold heating oven,
- Coaxial current input,
- Sliding current input,
- Crucible rotation mechanism,
- Vacuum system,
- Argon inlet system,
- Water cooling system,
- Pneumatic system,
- Power cabinet,
- Capacitor battery,
- Control system cabinet,
- Service platform,
- Power supply "TPCHT-250".
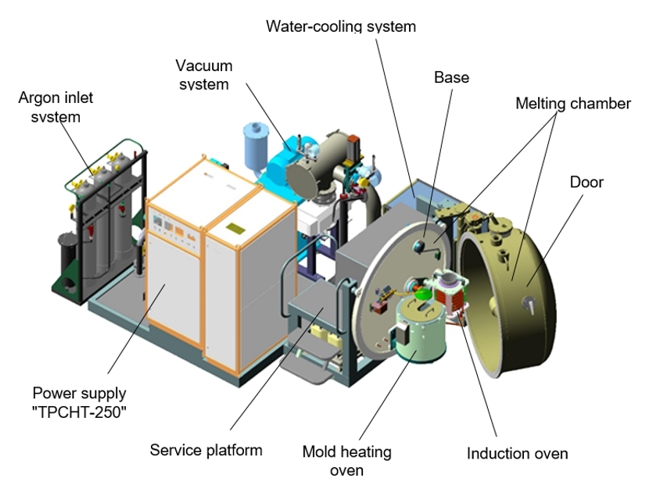
The "VIPE-3R" plant has a modular structure: replaceable melting furnaces, replaceable mold heating furnaces, replaceable crucibles. The capacity of replaceable steel melting furnaces is 18 kg. The plant can fill up to four molds per hour.
3.1. Melting chamber.
The melting chamber is the main element of the plant and consists of a base and a door.
The base is made of stainless steel, located in a vertical plane, and has external water cooling. The current conductor, inductor and mold heating oven are attached to the base using brackets. The induction furnace assembly consists of a replaceable inductor, a crucible and a ramming system.
The base also has a number of pressure seals for various purposes and a vacuum pipe connecting the melting chamber to the vacuum system.
There are two limit switches on the base flange, the state of which indicates that the induction furnace is in a vertical position when loading with metal (charge) and melting, or the metal is being drained into the mold.
The limit switches are triggered by the operation of the crucible rotation mechanism - the gear motor and gear transmission.
Operator controls the speed of metal spill.
3.2. Door.
The door is a welded structure of a cylindrical shape, bounded by a flange on one side and a torispherical bottom on the other. The door body is made of stainless steel, has a water-cooled cavity, a pipe for a safety valve, a pipe for inserting an immersion thermocouple and two viewing windows for visual monitoring of the process.
3.3. Induction oven.
An induction melting furnace is designed to melt heat-resistant metal and pour it into shell molds.
The working part of the furnace is an inductor of a rectangular copper tube. The induction furnace is mounted on a rotating bracket. There is an opportunity to adjust the height and trajectory of the drain.
Thyristor frequency converter “TPCHT-250” and a capacitor battery supply the power to the melting furnace through water-cooled copper busbars.
3.4. Mold heating oven.
The mold heating furnace provides the required temperature conditions for the pre-heating of the molds.
The mold heating oven is installed on a bracket, which is mounted on the inner plane of the base. The furnace bracket is in a stationary position relative to the induction furnace. The power supply conductors are inserted into the mold heating oven through special pins located in the sealed leads of the base housing. There is a hole in the body of the mold heating furnace through which thermocouples are introduced into the internal space of the mold heating furnace to measure temperature.
3.5. Coaxial current lead.
The coaxial current lead is designed to transfer electricity to the melting inductor from a sliding current lead. The crucible rotation mechanism rotates the coaxial current lead. The crucible rotation mechanism consists of a gear motor and a set of gears. The current lead is water-cooled. Cooling water pressure is 0.2 MPa or more.
3.6. Sliding current lead.
The sliding current lead is designed to transmit electricity from a capacitor battery through a coaxial current lead to an induction furnace and ensure metal melting in it. It consists of two housings isolated from each other, mounted on a coaxial current supply. The current lead is water-cooled.
3.7. Vacuum system.
The vacuum system provides a given value of residual pressure in the melting chamber and the additional loading chamber. The system components are made of stainless steel. The cut-off equipment has pneumatic and electromechanical drives.
Vacuuming is carried out through a technological vacuum valve with the opened sealing valve. The pressure in the melting chamber is monitored by a vacuum gauge. A steam-oil booster pump is used to achieve a deep vacuum.
3.8. Argon inlet system (optional).
The argon inlet system is designed for accelerated cooling of castings.
Purified argon is supplied from the inlet ramp into the melting chamber under atmospheric pressure or less when the metal is melted and poured into the mold.
There is a vacuum gauge on the flange of the melting chamber, with which the argon pressure in the chamber is monitored.
3.9. Water cooling system.
The water cooling system is designed to cool all elements operating in high temperature zones or creating high temperatures. The system consists of pipelines, water flow and supply sensors, temperature sensors, and has a sound and light alarm. The cooling system components are made of stainless steel.
3.10. Pneumatic system.
The purpose of the pneumatic system is to open and close the gates and valves of the vacuum system, movement mechanisms, the pressure of the compressed air supplied to the plant is at least 6.3 bar.
The requirement is simplicity and reliability of design, ease of repair and operation. Equipped with a filter-moisture separator
3.11. Thyristor converter "TPChT-250"
The thyristor power supply meets modern requirements of metallurgical and foundry equipment.
The converter cabinet is a frame system made of a special profile. The sides of the cabinet are closed with removable walls, and the front and rear sides have doors for access to the main elements of the converter. On the front side of the cabinet there is a panel with instruments and controls. The converter has the ability to connect a remote control. A control system, power chokes, a protection panel, a starting unit, a rectifier unit, an inverter unit and a cooling system are mounted inside the cabinet. The power supply has a water cooling system.
The "VIPE-3R" plant is intended for the manufacturing castings from heat-resistant alloys and steels in mass production conditions. Casting method - lost wax casting. The range of castings includes equiaxial, small-sized, shaped and body parts made of heat-resistant alloys and steels. Casting block dimensions are up to 370 mm.
2. Features of the physical processes used.
Features of the "VIPE-3R" plant - a single-chamber plant, the ability to fill up to four molds per hour. The temperature of the metal is controlled by pyrometer within the melting process. Data from photopyrometer and immersed thermocouple pass to the monitor. The physical process is a result of magnetic induction.
3. Technical description. Design features. Advantages.
The "VIPE-3R" plant includes the following main components:
- Melting chamber,
- Door,
- Induction oven,
- Mold heating oven,
- Coaxial current input,
- Sliding current input,
- Crucible rotation mechanism,
- Vacuum system,
- Argon inlet system,
- Water cooling system,
- Pneumatic system,
- Power cabinet,
- Capacitor battery,
- Control system cabinet,
- Service platform,
- Power supply "TPCHT-250".
The "VIPE-3R" plant has a modular structure: replaceable melting furnaces, replaceable mold heating furnaces, replaceable crucibles. The capacity of replaceable steel melting furnaces is 18 kg. The plant can fill up to four molds per hour.
3.1. Melting chamber.
The melting chamber is the main element of the plant and consists of a base and a door.
The base is made of stainless steel, located in a vertical plane, and has external water cooling. The current conductor, inductor and mold heating oven are attached to the base using brackets. The induction furnace assembly consists of a replaceable inductor, a crucible and a ramming system.
The base also has a number of pressure seals for various purposes and a vacuum pipe connecting the melting chamber to the vacuum system.
There are two limit switches on the base flange, the state of which indicates that the induction furnace is in a vertical position when loading with metal (charge) and melting, or the metal is being drained into the mold.
The limit switches are triggered by the operation of the crucible rotation mechanism - the gear motor and gear transmission.
Operator controls the speed of metal spill.
3.2. Door.
The door is a welded structure of a cylindrical shape, bounded by a flange on one side and a torispherical bottom on the other. The door body is made of stainless steel, has a water-cooled cavity, a pipe for a safety valve, a pipe for inserting an immersion thermocouple and two viewing windows for visual monitoring of the process.
3.3. Induction oven.
An induction melting furnace is designed to melt heat-resistant metal and pour it into shell molds.
The working part of the furnace is an inductor of a rectangular copper tube. The induction furnace is mounted on a rotating bracket. There is an opportunity to adjust the height and trajectory of the drain.
Thyristor frequency converter “TPCHT-250” and a capacitor battery supply the power to the melting furnace through water-cooled copper busbars.
3.4. Mold heating oven.
The mold heating furnace provides the required temperature conditions for the pre-heating of the molds.
The mold heating oven is installed on a bracket, which is mounted on the inner plane of the base. The furnace bracket is in a stationary position relative to the induction furnace. The power supply conductors are inserted into the mold heating oven through special pins located in the sealed leads of the base housing. There is a hole in the body of the mold heating furnace through which thermocouples are introduced into the internal space of the mold heating furnace to measure temperature.
3.5. Coaxial current lead.
The coaxial current lead is designed to transfer electricity to the melting inductor from a sliding current lead. The crucible rotation mechanism rotates the coaxial current lead. The crucible rotation mechanism consists of a gear motor and a set of gears. The current lead is water-cooled. Cooling water pressure is 0.2 MPa or more.
3.6. Sliding current lead.
The sliding current lead is designed to transmit electricity from a capacitor battery through a coaxial current lead to an induction furnace and ensure metal melting in it. It consists of two housings isolated from each other, mounted on a coaxial current supply. The current lead is water-cooled.
3.7. Vacuum system.
The vacuum system provides a given value of residual pressure in the melting chamber and the additional loading chamber. The system components are made of stainless steel. The cut-off equipment has pneumatic and electromechanical drives.
Vacuuming is carried out through a technological vacuum valve with the opened sealing valve. The pressure in the melting chamber is monitored by a vacuum gauge. A steam-oil booster pump is used to achieve a deep vacuum.
3.8. Argon inlet system (optional).
The argon inlet system is designed for accelerated cooling of castings.
Purified argon is supplied from the inlet ramp into the melting chamber under atmospheric pressure or less when the metal is melted and poured into the mold.
There is a vacuum gauge on the flange of the melting chamber, with which the argon pressure in the chamber is monitored.
3.9. Water cooling system.
The water cooling system is designed to cool all elements operating in high temperature zones or creating high temperatures. The system consists of pipelines, water flow and supply sensors, temperature sensors, and has a sound and light alarm. The cooling system components are made of stainless steel.
3.10. Pneumatic system.
The purpose of the pneumatic system is to open and close the gates and valves of the vacuum system, movement mechanisms, the pressure of the compressed air supplied to the plant is at least 6.3 bar.
The requirement is simplicity and reliability of design, ease of repair and operation. Equipped with a filter-moisture separator
3.11. Thyristor converter "TPChT-250"
The thyristor power supply meets modern requirements of metallurgical and foundry equipment.
The converter cabinet is a frame system made of a special profile. The sides of the cabinet are closed with removable walls, and the front and rear sides have doors for access to the main elements of the converter. On the front side of the cabinet there is a panel with instruments and controls. The converter has the ability to connect a remote control. A control system, power chokes, a protection panel, a starting unit, a rectifier unit, an inverter unit and a cooling system are mounted inside the cabinet. The power supply has a water cooling system.
Technical data
Power supply voltage, V
400
Frequency, Hz
50
Phases
3
Power source power, kW
250
Crucible capacity for steel, kg
18
Residual pressure in a cold furnace, mmHg
1*10-4
Melting pressure, mmHg
5*10-3 to 5*10-2
Pouring pressure, mmHg
5*10-3 to 5*10-2
Leakage (with a cold crucible), l µm. Hg/sec
5
Mold productivity/hour
4
Argon pressure in the operating environment, mmHg
300
Liquid metal temperature, °C
1400 to 1700
Preheating of molds
yes
Maximal mold temperature, °C
1100
Maximal mold heating speed,°C/min
50
Dimensions of the PPF muffle (Ø internal, Ø external, height), mm
420;310*425
Dimensions of the poured ceramic block of molds (Ø*H), mm
300*420
Internal dimensions of the crucible (Ø*H), mm
140*270
External dimensions of the crucible (Ø*H), mm
170*300
Crucible rotation speed (pouring speed)
adjustable
Maximal tilt angle of the melting furnace crucible (forward, backward), degrees
+110; -15
Holding time of the poured mold in vacuum, minutes
10
Dimensions (L*W*H), mm
4000*3500*3000
Weight, kg
5800
Detailed information PDF
Video
Submit an inquiry
Прошлое
Настоящее
Будущее